Skip to content
Three and four stations

One-step injection stretch blow molding (ISBM) machines

Three-station and four-station injection stretch blow molding (moulding) for a range of plastic containers.

One-step ISBM
Process
3 / 4
Stations
2 options
Options
By bottle
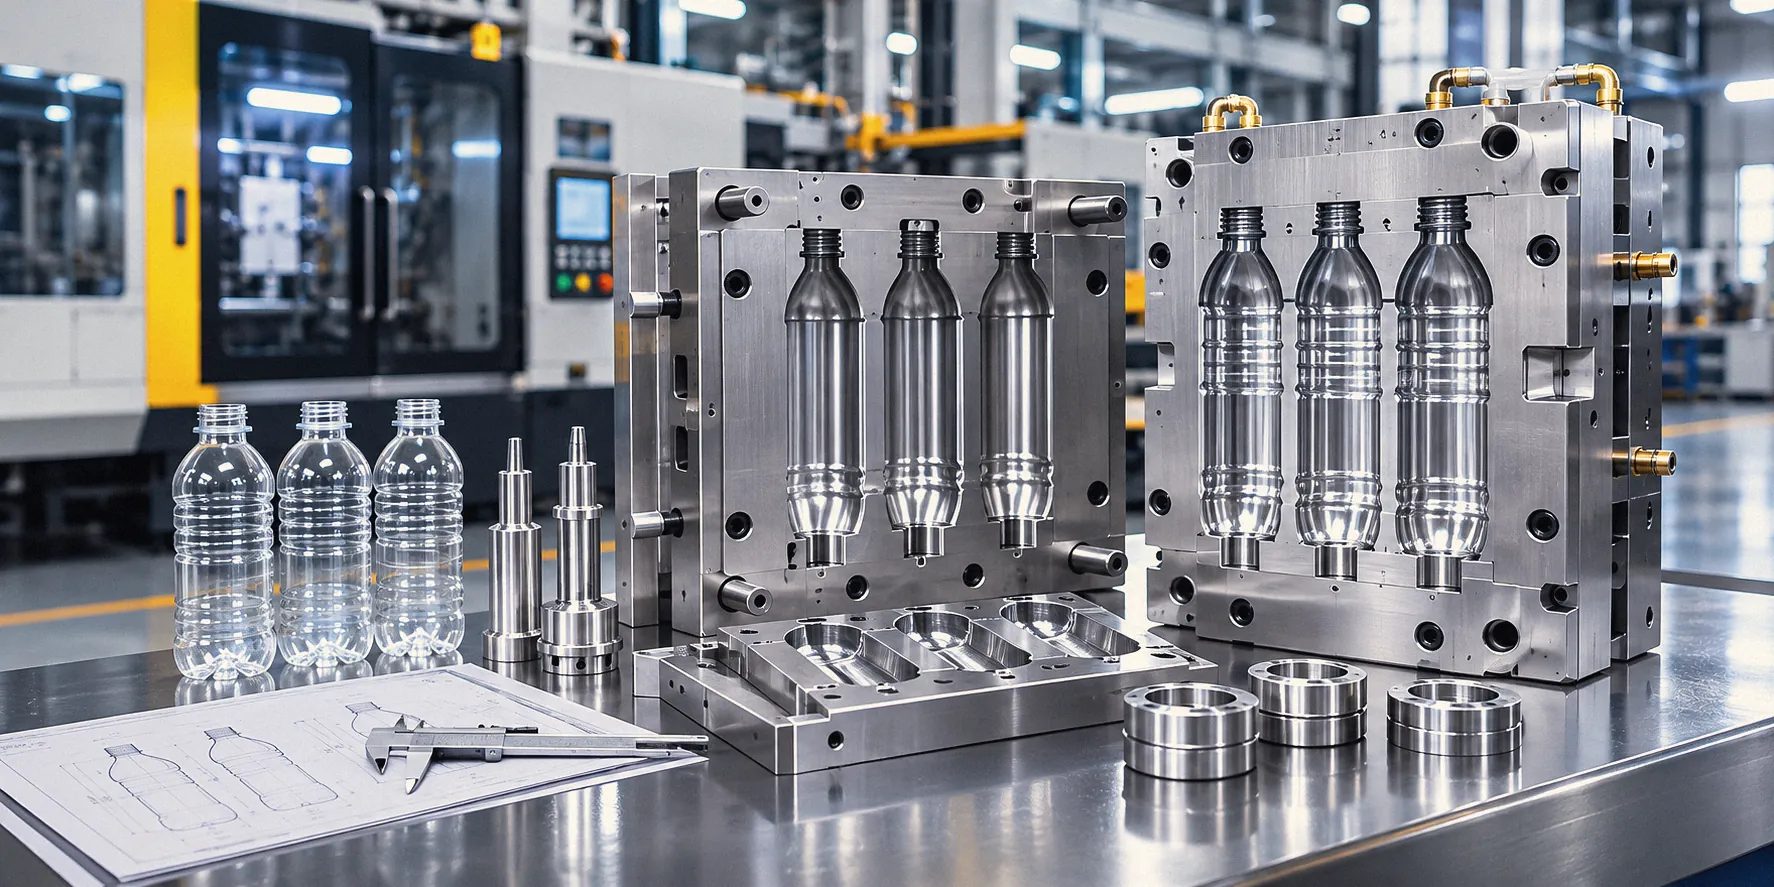
Tooling
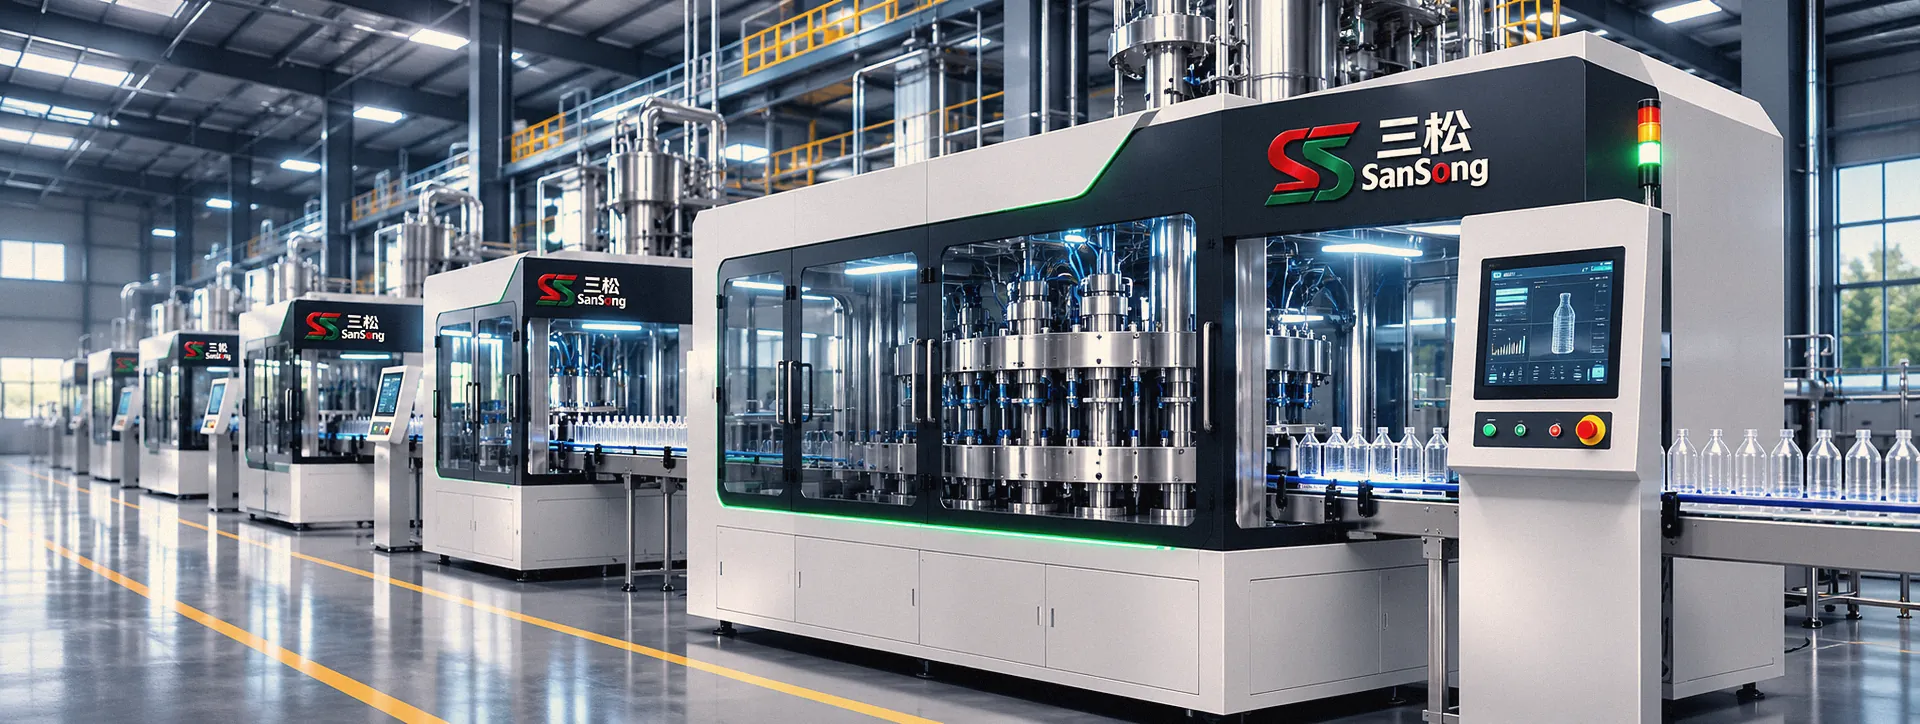
White and black SanSong one-step ISBM machines in a factory, with glass guards, a control panel and bottles on the outfeed

From resin to a finished container

SanSong supplies one-step injection stretch blow molding machines and molds. The range includes three-station standard and two-colour machines, plus a four-station double-row machine.

The three-station process combines preform injection, stretch blow molding and removal. The four-station layout includes a separate conditioning stage.

Applications presented by SanSong include sports bottles, baby feeding bottles, food and beverage containers, pharmaceutical packaging and cosmetic packaging.

Choose by container and material

Start with the bottle volume, weight, shape, neck finish and material grade. The intended output and cavity arrangement guide the machine and mold selection.

SanSong lists PET, RPET, PETG, PC, PP, PPSU, AS, PS, PMMA, HDPE, Tritan and ECOZEN among its material applications. Suitability needs confirmation for the chosen grade and container.

A process selected for your bottle

The published machine families include a three-station standard model, a three-station two-colour model and a four-station double-row model. Request the current machine specification and discuss sample trials. Output, cycle time and energy use depend on the selected product and process.

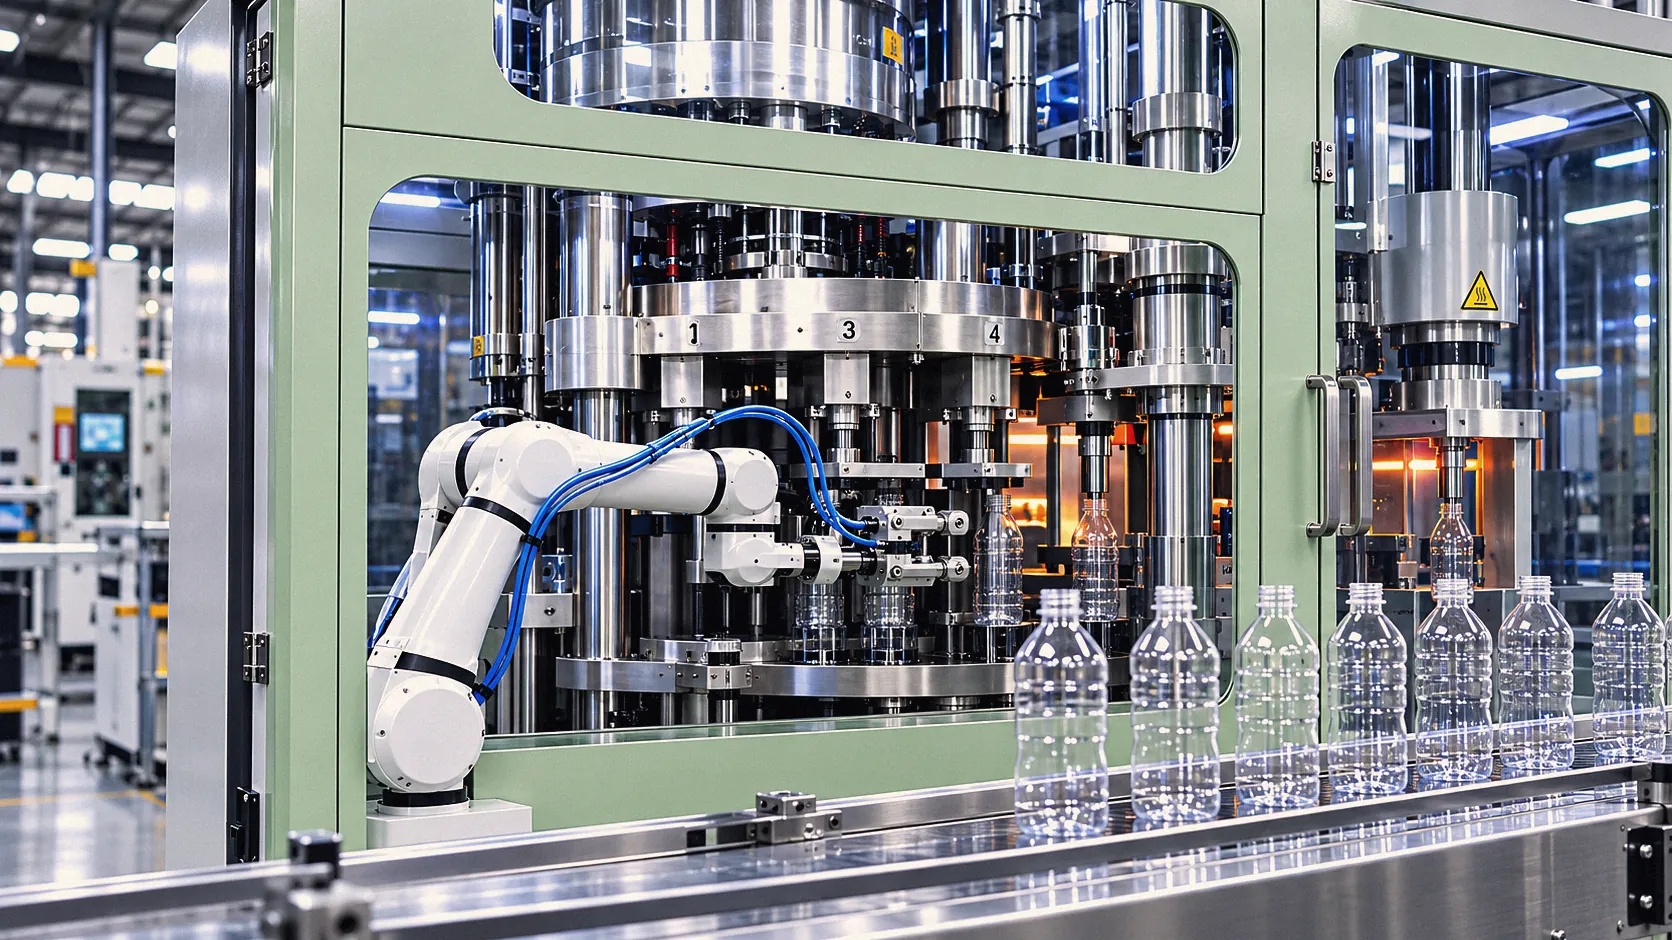
SanSong one-step ISBM take-out cell, with station numbers and bottles on the conveyor

Machine and mold, considered together

A complete enquiry includes the container drawing or sample, material, required output and available utilities. Include any existing mold or machine information.

The two-colour option serves container appearance requirements; the double-row configuration offers a different tooling layout. The engineering review determines which is suitable.

Bottle handling, removal and downstream operations should be discussed as part of the production layout.

Move from samples to production

Agree the trial material, sample inspection criteria and project documentation before finalising the equipment scope.

Food, baby-care and pharmaceutical packaging requirements depend on the material, application and market. Equipment selection alone does not establish product compliance.

Contact the ISBM team for the current technical data, tooling discussion and project quotation.

THE MACHINE RANGE

Three machines, one process.

Every SanSong ISBM machine turns resin into a finished container on one machine. Choose the configuration by the container you need to make.

Three-station standard machine

Preform injection, stretch blow molding and container release in three stations. The preform moves straight from injection to blowing while it still holds its injection heat. Built for transparent containers such as sports bottles, baby feeding bottles and juicer bottles.

Stations
3
Colours
Single colour
Published resins
PC, PCTG (Tritan TX1001 / TX2001, ECOZEN YF300 / T110 / T110 Pro), AS, PPSU

Three-station two-colour machine

Two independent single-cylinder injection units, each with its own pressure and speed control, feed a colour-mixing hot runner. The layout is designed to reduce the visible line where the two colours meet, and to help prevent short shots and uneven walls. With one injection unit switched off, the machine runs single-colour containers.

Stations
3
Colours
Two-colour or single colour
Typical use
Household and beauty packaging

Four-station double-row machine

A separate conditioning station sits between injection and blowing, so each preform is heated or cooled to the temperature the process needs. The double-row mold layout uses the mold area fully for high-volume, single-colour containers on a small footprint. An optional tail-cutting device trims the PET preform gate for a cleaner, brighter bottle base.

Stations
4
Mold cavities
8–24
Typical use
PET containers in volume, such as syrup bottles
BLENDER 3D MECHANICAL ARCHITECTURE

3D Rotary Turret Architecture: Indexing, Clamping & Telemetry

Modeled and animated in Blender 4.2 with orthographic CAD contours to clarify clamping, gear-driven indexing, and closed-loop process telemetry alongside real factory documentation.

3D Engineering Process Schematic
Isometric Ortho · 1–12 Cavities · Up to 4.6 L Scope
SCENE 01 · ONE-STEP ROTARY ISBM ARCHITECTURE

Multi-Station Rotary Indexing, Split Blow Clamping & Telemetry

Isometric Blender 4.2 3D schematic illustrating how preform thermal conditioning, radial split blow-mold clamping, vertical stretch-rod actuation, and closed-loop HMI telemetry coordinate within one continuous cycle.

  • Preform Conditioning Dial: Retains residual injection heat through segmented thermal shields before blow transfer.
  • Radial Split Blow Clamping: Indexed clamping carriages lock split steel mold cavities symmetrically around the container axis.
  • Servo Stretch-Blow Stroke: Overhead stretch rod and pneumatic manifold synchronize axial stretch with high-pressure blow air.
  • SPC Process Telemetry: Cycle timing, core displacement, and manifold pressure report to the operator HMI screen.

Kinematic principle model; actual 3-station or 4-station turret geometry follows your confirmed SS-400 model.

Discuss container drawing
30-SECOND CHIEF-ENGINEER SELECTOR · 2026 VERIFIED LINEUP

Interactive 30-Second One-Step ISBM Model & Station Selector

Filter all 8 Liuzhou-built one-step ISBM platforms by container geometry, thermal conditioning need, clamping force, or changeover architecture. Every figure comes strictly from published SanSong specifications and EU Digital Product Passports.

Showing 8 of 8 published ISBM models

SanSong 8-Model One-Step ISBM Specifications and Prefilled RFQ Links
Model CodeStations & ArchitectureClamping / CavitiesPower / Weight / FootprintVerified Application & Resin NotesEU DPP1-Click Prefilled RFQ
SS-400-60-03-013-station · Single-row, single-color1–12 cavities · Up to 4.6 L · Clamping on datasheet74 kW · 11,500 kg · 4,980 × 2,100 × 3,450 mmPC, PCTG (Tritan/ECOZEN), PET, RPET, PETG, AS, PPSU, PP, PMMA, HDPE; sports bottles, baby feeding bottles, pharma & plasma cups; domestic mold interface review.View DPP ↗Quote SS-400-60-03-01 →
SS-400-60-03-023-station · Dual-injection two-color / single-colorScrews 65 / 45 mm · Core lift ≤ 1 m/s · Cavities per mold80 kW · 12,000 kg · 5,050 × 2,100 × 3,450 mm2 independent injection units + color-mixing hot runner + German ECKERLE gear pump + magnetic core-position sensing; runs single-color molds with one unit off.View DPP ↗Quote SS-400-60-03-02 →
SS-400-60-03-033-station · Single-color, quick blow-mold changeConfirmed per mold & container · Quick-change blow frame74 kW · Weight per config · 4,980 × 2,100 × 3,450 mmUpgraded rapid blow-mold changeover mechanics for multi-SKU personal care and bottle plants; compatible with Japanese benchmark molds after interface drawing review.View DPP ↗Quote SS-400-60-03-03 →
SS-500-60-03-043-station · Single-color, enlarged shot volumeEnlarged injection shot capacity · Cavities per mold74 kW · 11,500 kg · 4,980 × 2,100 × 3,450 mmDerived from SS-400-60-03-03 with enlarged injection shot volume for heavy-grammage cosmetic jars, thick-base bottles, and wide-belly food containers.View DPP ↗Quote SS-500-60-03-04 →
SS-400-80-03-053-station · Single-color, 80-ton injection clamping80-ton injection clamping force · Cavities per mold82.8 kW · 12,000 kg · Dimensions per configurationUpgraded 80-ton injection clamping tonnage resisting parting-line flash across multi-cavity wide-mouth jars, pharmaceutical packers, and large projected neck areas.View DPP ↗Quote SS-400-80-03-05 →
SS-400-60-03-063-station · Two-color + quick mold changeDual injection + quick-change blow frame · Per mold80 kW · 12,000 kg · 4,980 × 2,050 × 3,450 mmCombines SS-400-60-03-02 two-color gradient capability with SS-400-60-03-03 rapid mold changeover and benchmark mold interface adaptability.View DPP ↗Quote SS-400-60-03-06 →
SS-400-60-04-014-station · Single-row + dedicated conditioning1–12 cavities · Dedicated preform thermal conditioning74 kW · 18,000 kg · 5,800 × 2,100 × 3,500 mm Dedicated 2nd-station thermal conditioning equalizes preform core/skin heat for thick-wall cosmetic PETG, asymmetric/oval profiles, small & wide necks; optional PET tail-cutting.View DPP ↗Quote SS-400-60-04-01 →
SS-400-110-04-024-station · Double-row + conditioning8–24 cavities (incl. 1-out-24 lamp cover / small-bottle molds)90 kW · 17,000 kg · 5,800 × 2,100 × 3,450 mmDouble-row mold layout with 3 Delta servo sets & Delta HMI touch screen for high-cavity PET syrup, pharma, and 24-cavity PC/PMMA lamp cover runs; optional PET tail-cutting.View DPP ↗Quote SS-400-110-04-02 →
PUBLISHED SPECIFICATION

Three-station standard machine.

Reference values SanSong publishes for its three-station single-colour machine. Values listed as on request depend on the configuration. Your quotation confirms the data for your machine.

Machine data
ParameterValue
Screw diameterØ65 mm (standard)
Screw speed0–150 r/min
Maximum hydraulic pressure17.5 MPa
Blowing air pressure and flow3.0 MPa · 1,340 L/min
Machine air pressure and flow1.0 MPa · 460 L/min
Cooling water pressure0.2–0.3 MPa
Machine dimensions4,980 × 2,100 × 3,450 mm
Machine weight11,500 kg
Injection capacity, injection rate, clamping forces, servo power, heater capacityOn request
Largest container by cavity count
CavitiesThread diameterBody diameterMaximum heightMaximum weight*
1107 mm150 mm335 mm430 g
290 mm150 mm335 mm215 g
3 to 12On requestOn requestOn requestOn request

*Container weight is calculated with the density of PC.

SanSong may adapt the specification to a project. The figures in your quotation apply.

TECHNICAL CONFIGURATION

What goes into the machine.

The main assemblies of SanSong’s one-step ISBM machines, as published by SanSong.

Injection unit

Single-cylinder injection keeps the unit compact, easy to maintain and quick to service. A 1,000 cc/rev hydraulic melt motor gives the torque for viscous, high-fill resins. Back pressure is set on the touch screen through a proportional electro-hydraulic valve, barrel temperatures run under PID control, and the unit moves on twin linear guides.

Injection clamping

Hydraulic-cylinder clamping works with a servo system and four large-diameter tie bars. The rotary table is driven by a motor coupled directly to the reducer, with no gear train, and reports its position back to the control.

Blow clamping

Two differentially connected hydraulic cylinders close the blow mold. The generous mold area accepts molds with different cavity counts.

Servo hydraulics

Energy-saving servo drives: Delta servo motors with high-speed ECKERLE gear pumps made in Germany, under a Delta electro-hydraulic servo controller for fast, precise motion.

Control system

A Delta PLC with optional remote programme maintenance, a 10-inch Delta touch screen with Chinese and English menus, and non-contact magnetic displacement sensors that have no wearing contacts.

MANUFACTURER, SCOPE & QUOTATION FACTORS

What determines ISBM machine price — and how SanSong builds the line.

Liuzhou Sansong Automation Technology Co., Ltd. (SanSong, USCC 914502000674272010), founded in 2013 in Liuzhou, Guangxi, China, operates a 9,336 m² facility with 121 employees, 10 invention patents and 33 utility model patents, under ISO 9001:2015 (Cert. No. 11426Q00192R201, valid 2026-01-23 to 2029-01-22) covering R&D, production and sale of hollow forming equipment and non-standard automatic devices. SanSong quotes every machine around the actual container rather than publishing generic list prices.

Six factors that determine an ISBM quotation

ISBM quotation cost drivers
Quotation FactorHow It Shapes the Configuration & Offer
1. Station layout & machine modelChoosing among 3-station standard (SS-400-60-03-01), 2-color (-03-02 / -03-06), quick-change (-03-03), enlarged shot (-03-04), 80-ton wide-neck (-03-05), or 4-station single/double-row (-04-01 / -04-02).
2. Container geometry & cavity countContainer volume, gram weight, neck finish, shape (round, wide-neck, handled, inner-thread) and cavity count set clamping force, shot size and mold frame dimensions.
3. Resin grade & temperature controlRunning PET, RPET, PETG, PC, PCTG (Tritan / SK ECOZEN), PPSU, PP, AS, PS, PMMA or HDPE determines drying dew point, screw/barrel configuration and water/oil mold heating.
4. Complete ISBM mold set & hot runnerIncludes preform cavities, injection cores, neck molds, blow molds, ejection tooling, hot runner (single or color-mixing) and conditioning pots on 4-station lines.
5. Auxiliaries & downstream automationOptional dehumidifying dryer & loader, chiller, air compressor, mold dehumidifier, plus take-out robot, pick-and-place robot, leak testing, vision inspection, packing and palletizing.
6. Utilities, electrical options & deliveryLocal voltage/frequency, European-standard electrical configuration on request, pre-shipment sample scope, installation/training and destination shipping terms.

Core component brands, auxiliaries & downstream bottle automation

Verified component suppliers and line scope
System AreaPublished SanSong Configuration Scope (April 2026 Brochures)
Core component brands used in assembliesDelta / Inovance (servo drives & HMI), ECKERLE gear pump, GEFRAN sensors, YUKEN hydraulic valves, Schneider Electric switchgear, AirTAC pneumatic components, Parker solenoid valves and Germanjet magnetic displacement sensors. (Component brands used in machine builds; not brand endorsements.)
Published resin rangePET, RPET, PETG, PC, PCTG (Tritan TX1001/TX2001, SK ECOZEN YF300/T110/T110Pro), PP, PPSU, AS, PS, PMMA and HDPE (final suitability confirmed per grade and trial).
4 auxiliary equipment familiesRaw Material Dehumidifying Dryer & Loader · Chiller · Air Compressor System · Mold Dehumidifier.
6 downstream bottle automation optionsTake-out Robot · Pick-and-Place Robot · Leak Testing Machine · Vision Inspection System · Empty Bottle Packing Machine · Automatic Palletizing Robot.

9-item ISBM pre-selection checklist (what to prepare before quoting)

  • Container 2D/3D drawing or physical sample bottle
  • Nominal capacity (mL / L) and target gram weight
  • Neck finish diameter, thread style (incl. inner-thread) and closure
  • Exact resin grade, color (single or two-color gradient) and end-use market
  • Hourly or annual production output target
  • Station preference (3-station vs 4-station conditioning or double-row) if known
  • Existing molds to check for compatibility (interface drawing if applicable)
  • Local power voltage, phase and frequency (50 Hz / 60 Hz)
  • Auxiliary machines and downstream automation needed (dryer, chiller, compressor, take-out robot, inspection/packing)

Related engineering insights

COMPLETE 8-MODEL ISBM LINEUP (2026)

Compare all 8 SanSong one-step ISBM machine models.

SanSong (Liuzhou Sansong Automation Technology Co., Ltd.) builds 8 one-step injection stretch blow molding models in Liuzhou — 2 four-station machines and 6 three-station machines. Values below come directly from SanSong’s April 2026 brochures; parameters that vary by configuration or require engineering verification are explicitly marked.

SanSong 8-Model One-Step ISBM Specification Matrix (April 2026)
ModelStations & LayoutCavities / ClampingInstalled Power (50 Hz)WeightDimensions (L × W × H mm)Key Positioning
SS-400-60-04-014-station · Single-row, single-color1–12 cavities · Clamping on datasheet74 kW18,000 kg5,800 × 2,100 × 3,500Medium-output flexible production (small- & wide-neck); conditioning station; optional PET tail-cutting
SS-400-110-04-024-station · Double-row, single-color8–24 cavities · Clamping on datasheet90 kW17,000 kg5,800 × 2,100 × 3,450Space-saving double-row layout for volume production; Delta servos & HMI; optional PET tail-cutting
SS-400-60-03-013-station · Single-row, single-color1–12 cavities · Up to 4.6 L74 kW11,500 kg4,980 × 2,100 × 3,450Standard single-cylinder model; compatible with similar domestic molds (subject to interface review)
SS-400-60-03-023-station · Two-color & single-colorConfirmed per mold · Screws 65 / 45 mm80 kW12,000 kg5,050 × 2,100 × 3,450Dual independent injection units + color-mixing hot runner; runs single-color by switching off one unit
SS-400-60-03-033-station · Single-color, quick mold changeConfirmed per mold & container74 kWConfirmed per configuration4,980 × 2,100 × 3,450Upgraded rapid blow-mold change; compatible with Japanese benchmark molds (subject to interface review)
SS-500-60-03-043-station · Single-color, large shot volumeConfirmed per mold & container74 kW11,500 kg4,980 × 2,100 × 3,450Derived from -03-03 with enlarged injection shot volume for heavier-weight and thicker-wall containers
SS-400-80-03-053-station · Single-color, 80-ton clamping80-ton injection clamping · Cavities per mold82.8 kW12,000 kgConfirmed per configurationUpgraded 80-ton injection clamping force specifically for high-output wide-neck containers
SS-400-60-03-063-station · Two-color + quick mold changeConfirmed per mold & container80 kW12,000 kg4,980 × 2,050 × 3,450Combines -03-02 color-mixing performance with -03-03 mold compatibility (with mixing hot runner) and quick change

Note: Clamping force (other than 80 tons published for SS-400-80-03-05), shot size, cycle time, utility consumption, and European-standard electrical configuration options are confirmed on the configuration datasheet issued with your written quotation.

HONEST PROCESS BOUNDARY DISCLOSURE · CHIEF-ENGINEER REVIEW

When One-Step ISBM Wins — And When Another Process Is Better

WHEN ONE-STEP ISBM WINS

Precision Neck Finish + Zero-Scuff Biaxial Clarity

  • Precision injection-molded neck finishes (threads, wiper necks, snap rings, non-forced inner-thread cups) formed in the same thermal cycle as biaxially stretched walls.
  • Zero preform cold storage, gaylord dumping, or reheat-conveyor ring scuffing — preserving optical surface gloss on thick-wall PETG/AS/PMMA cosmetic jars and droppers.
  • Proven across PPSU/PP baby feeding bottles, wide-mouth pharma packers, apheresis plasma separation cups, Tritan/PCTG/PC sports bottles (up to 4.6 L on SS-400-60-03-01), and two-color vessels (SS-400-60-03-02 / -03-06).
  • Thick-wall or oval/asymmetric profiles step up to 4-station thermal conditioning (SS-400-60-04-01 single-row 1–12 cavities or SS-400-110-04-02 double-row 8–24 cavities).
HONEST PROCESS & CHANGEOVER BOUNDARIES

Where Two-Stage SBM or EBM Wins & Changeover Realities

  • High-speed single-SKU commodity water & CSD lines (> 15,000 bph): Rotary two-stage reheat stretch blow molding achieves lower unit conversion cost when bulk preform transport marks are acceptable; SanSong builds integrated one-step ISBM only.
  • Hollow handleware & automotive pinch-off ducts: Containers requiring integral hollow grab-handles, industrial jerrycans, or parison pinch-off seams belong on extrusion blow molding (EBM); we disclose this upfront during drawing review.
  • Short-run full-mold changeover reality: One-step SKU switches swap injection cavities, core rods, blow molds, and neck rings together — multi-SKU plants should specify quick-change SS-400-60-03-03 or SS-400-60-03-06 and standardize neck finishes.
  • Dual-barrel two-color purge planning: Switching dark-to-light pigments or resins across the dual-unit mixing hot runner on SS-400-60-03-02 / -03-06 requires scheduled barrel purge resin and thermal stabilization minutes.
UNIT ECONOMICS FAT WORKSHEET & CONTAINER FMEA DIAGNOSTICS

Unit Economics FAT Verification Metrics & 5-Defect ISBM FMEA Matrix

Instead of generic industry benchmark claims, SanSong structures Factory Acceptance Testing (FAT) around three directly metered shop-floor economics indicators and a five-mode defect countermeasure matrix.

FAT · 01

Specific Energy (kWh / 1,000 Accepted Containers)

Logged across steady-state Liuzhou FAT cycles on your exact resin and cavity count (1–12 or 8–24 cavities across 74–90 kW 50 Hz rated platforms), metering press servo-hydraulics, hot-runner zones, resin dryer, mold chiller, and high-pressure air together rather than quoting generic nameplate fractions.

FAT · 02

First-Pass Yield & Zero Preform Tray Scrap

Calculated as dimensionally & visually accepted containers divided by total injected shots over continuous multi-hour FAT runs — capturing the elimination of two-stage preform cold-storage moisture regain, gaylord scuffing rejects, and reheat-oven drop-off scrap.

FAT · 03

Net Mold-Changeover Floor-to-Floor Minutes

Measured from the last accepted bottle of SKU A to the first QC-passed bottle of SKU B — separating mechanical hoist/clamp swap (standard SS-400-60-03-01 vs quick-change SS-400-60-03-03 / -03-06) from hot-runner thermal soak and barrel color-purge minutes.

5 Real One-Step ISBM Molding Defects, Root Causes, and SanSong Countermeasures
Container Defect ModeProcess / Tooling Root CauseSanSong 3/4-Station & Tooling CountermeasureAction
Body haze / spherulitic crystallizationPreform core/skin temperature sits too high entering stretch-blow or insufficient cooling rate on thick PET/PETG walls.Specify 4-station dedicated conditioning (SS-400-60-04-01 / SS-400-110-04-02) + optimize injection barrel & internal core-rod cooling zoning.4-Station Spec →
Pearlescence / stress whiteningPreform over-cooled below orientation window or stretch-rod advance mistimed relative to pre-blow pressure.Raise preform conditioning profile + synchronize servo stretch-rod curve and pre-blow delay (magnetic core-position sensing on -03-02).Preform Guide →
Circumferential wall eccentricityHot-runner manifold melt imbalance across cavities, core-rod circumferential temperature delta, or long-core deflection.Multi-zone independent hot-runner nozzle tuning + tapered neck-ring/core-rod concentricity lock machined in SanSong ISBM mold sets.Review Tooling →
Neck thread flash or sink marksClamping tonnage exceeded by wide-mouth multi-cavity projected area, or premature hold-pressure drop on thick neck rings.Step up to 80-ton clamping SS-400-80-03-05 for wide-neck containers + dedicated neck-ring chilled water circuit & multi-stage packing.Quote 80T Model →
Bottom gate vestige / pinholeHot-runner nozzle tip drooling/stringing or unconditioned crystalline gate slug resisting bottom center stretch.Match hot-runner gate land geometry to resin IV/MFR + optional automatic PET preform tail-cutting unit on 4-station -04-01 / -04-02.Defect Notes →
FAQ

Frequently asked questions

Useful details for your machine and mold enquiry.

What should I send for a bottle project?

Icon Close line

How do I choose three or four stations?

Icon Close line

Can you review an existing mold or machine?

Icon Close line

Which materials are listed by SanSong?

Icon Close line

Is a quoted cycle time valid for every bottle?

Icon Close line

How are trials and delivery arranged?

Icon Close line
Ready to automate your workflow?

Talk to our experts and discover the right solution for your production.